How does laser marking improve manufacturing efficiency? The answer begins with control. A focused beam can place serial numbers, barcodes, logos, and safety information directly onto metal, plastic, glass, or coated parts. It does not require ink, labels, plates, or physical contact. That removes several handling steps from the production line.
Laser marking specialist Dr. Reinhart Poprawe has described industrial lasers as enabling “flexible, fast, and precise processing.” His observation reflects what operators see beside a running machine. A clean mark appears within seconds. The part stays fixed. There is no drying time. There is less consumable waste. Digital files also allow quick design changes, which supports shorter product runs and greater customization.
The benefits extend beyond marking speed. Permanent codes can strengthen traceability, reduce manual recording, and help technicians identify parts during inspection. Automated vision systems can read consistent marks more reliably than handwritten labels. Maintenance may also become simpler because the process uses fewer replaceable materials.
Still, laser marking is not automatically efficient. Poor parameter settings can create weak contrast, heat damage, or unreadable codes. Reflective surfaces may require careful beam control. Operators need testing, training, and honest measurement. A faster mark means little if rejects increase.
The real gain comes from integration. When marking connects with software, inspection, and production data, it becomes part of the process rather than an isolated step. That is how does laser marking improve manufacturing efficiency in practical terms: fewer interruptions, clearer information, and more dependable production flow.
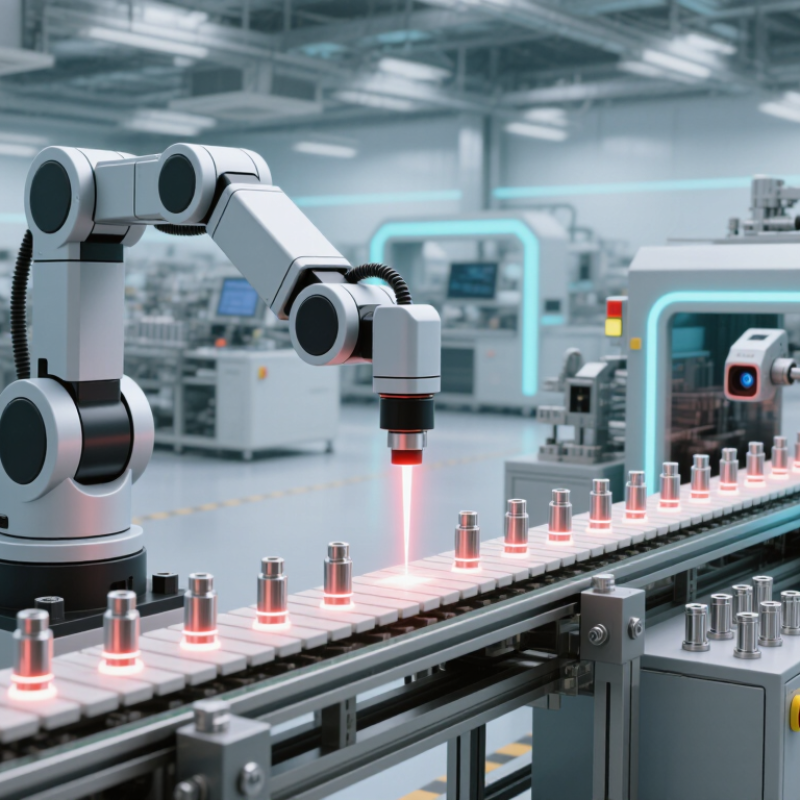
How Does Laser Marking Improve Manufacturing Efficiency?
Laser marking uses a focused light beam to change a material’s surface. The beam may remove, discolor, anneal, or engrave a controlled pattern. A scanner directs the beam across the part, while software controls position, speed, and power. No ink, labels, or physical cutting tools are required. That reduces consumables and routine tool replacement.
In practice, the process starts with a digital design and a calibrated work area. Operators can mark serial numbers, dates, barcodes, and traceability codes within seconds. The mark remains readable after handling, heat exposure, or cleaning when the settings match the material. The MarketsandMarkets Laser Marking Market report projects growth from about USD 3.1 billion in 2023 to USD 5.7 billion by 2028. This growth reflects demand for automated identification and flexible production, not guaranteed savings for every factory.
The efficiency gain is practical. A laser can switch between product codes without changing plates or waiting for ink to dry. Integrated vision systems can also verify contrast and position immediately. However, the first setting is rarely perfect. Reflective metals, curved surfaces, and heat-sensitive plastics require testing. Excessive power can create weak contrast or unwanted thermal damage. Engineers should record focal distance, pulse settings, and inspection results for repeatability. A poor setup can erase the promised efficiency. That is an important limitation.
| Efficiency Dimension | What Laser Marking Is | How It Works | Operational Data or Characteristic | Manufacturing Efficiency Benefit |
|---|---|---|---|---|
| Marking Method | A digital, computer-controlled process that creates text, codes, graphics, or identifiers directly on a workpiece. | A focused laser beam changes the surface through ablation, engraving, annealing, discoloration, or controlled material removal. | Non-contact and programmable | Reduces tooling changes and allows marking content to be updated through software rather than mechanical setup. |
| Consumables | Laser marking normally does not require ink, solvent, labels, screens, or physical marking dies. | Energy from the beam produces the mark directly on the material surface. | No marking ink or solvent during normal operation | Reduces consumable purchasing, replenishment, storage, and disposal activities. |
| Changeover | Marking patterns, serial numbers, dates, and product data can be selected digitally. | Control software sends a new marking file or variable data set to the laser system. | Software-based product changeover | Supports flexible production and reduces downtime associated with replacing physical plates, stamps, or screens. |
| Mark Permanence | The mark is integrated into or chemically changes the material surface rather than being applied as a removable label. | Laser energy produces a contrast change, surface engraving, or localized material transformation. | Permanent when the process is correctly matched to the material | Improves identification throughout manufacturing, assembly, inspection, service, and traceability operations. |
| Traceability | Laser systems can mark serial numbers, lot codes, barcodes, QR codes, and other machine-readable identifiers. | Variable information is generated from production, enterprise, or inspection data and applied in-line or at a workstation. | Supports unique, variable-data marking | Helps connect components with production records and reduces manual labeling and identification errors. |
| Marking Quality | Focused light enables precise marks on small areas and detailed geometries. | Beam position, pulse parameters, power, speed, and focus are controlled electronically. | High repeatability with digitally controlled parameters | Produces consistent identification and can reduce rework caused by illegible or incorrectly positioned marks. |
| Material Compatibility | Different laser wavelengths and configurations can be selected for metals, plastics, ceramics, glass, coated materials, and other substrates. | The selected wavelength and process parameters determine how the material absorbs the laser energy. | Material-specific process selection is required | Enables one production area to handle multiple materials when the system is properly configured and validated. |
| Contact and Wear | The marking head does not need to physically touch the workpiece. | The focused beam transfers energy across a working distance without a stamping tool or engraving bit. | No direct tool-to-part contact | Reduces contact-related tool wear and lowers the risk of scratching or deforming delicate parts. |
| Maintenance Profile | Many modern systems use solid-state or fiber-based laser sources with limited routine consumable requirements. | Routine work generally focuses on optics, ventilation, alignment, software, and process verification. | Fewer routine marking-tool replacements than mechanical methods | Can improve equipment availability, although preventive maintenance and safety inspections remain necessary. |
| Process Integration | Laser markers can be installed as stand-alone stations or integrated with conveyors, robots, vision systems, and production controls. | Signals and data are exchanged between the marking controller and the manufacturing system. | Suitable for automated and in-line workflows | Reduces manual handling and allows marking, verification, and data capture to occur within the production flow. |
| Inspection and Error Prevention | Laser marking can be paired with cameras or vision software to verify content, position, contrast, and readability. | The vision system compares the marked result with predefined acceptance criteria. | Automated verification is available | Helps identify incorrect or unreadable marks before parts move to later operations or shipment. |
| Environmental Considerations | The process can eliminate many ink, solvent, label, and backing-material requirements. | Material is modified directly by focused laser energy; extraction may be required for fumes or particles generated by some substrates. | Reduced marking-material waste, with process-specific extraction needs | Can lower waste from disposable marking supplies while supporting a cleaner and more controlled workstation. |
| Key Limitation | Laser marking is not automatically suitable for every material, color, geometry, or production environment. | Results depend on wavelength, power, pulse duration, focus, surface condition, motion control, and material response. | Application testing and parameter validation are essential | Proper qualification prevents poor contrast, excessive heat input, surface damage, and unreliable code readability. |
Note: Actual marking speed, contrast, depth, cycle time, and operating cost depend on the material, laser source, mark content, required quality, part geometry, automation level, and validated process parameters.
Laser marking uses a focused light beam to change a material’s surface. It can discolor, remove, anneal, or engrave controlled patterns. No ink or labels are needed.
It reduces drying time, label changes, solvent handling, and tool replacement. A programmed system can mark codes within seconds. Small delays disappear.
Common examples include serial numbers, dates, barcodes, and traceability codes. Digital files allow quick changes between product versions.
Suitable settings depend on the alloy, coating, finish, and geometry. Stainless steel may need annealed contrast. Coated aluminum may need coating removal.
Operators should identify the material and clean the surface. Dust, oil, and uneven clamping can distort the mark. A sample test is wise.
Cameras or trained operators inspect position, contrast, readability, and permanence. Tests may include wiping, abrasion, or environmental exposure. Inspection cannot rescue poor preparation.
It may reduce consumables, replenishment stops, relabeling, and rework. Savings are not guaranteed. Slow positioning or weak contrast can create new costs.
Reflective metals, curved surfaces, heat-sensitive plastics, and worn fixtures can cause variation. Excessive power may create thermal damage. The first setting is rarely perfect.
They should record focal distance, power, pulse duration, speed, frequency, and inspection results. These records support repeatability. Sometimes the real cause remains unclear.
No. Installation, testing, maintenance, and part positioning affect total cycle time. The cheapest system may not be the fastest one. Test before scaling.
Laser marking is a precise, contactless process that uses a focused laser beam to alter the surface of a material, creating permanent text, codes, symbols, or patterns. The process typically includes preparing the design, positioning the component, setting laser parameters, marking the surface, and inspecting the result. Because it can be automated and completed without inks, labels, or physical tools, it supports fast, consistent production with minimal setup and material waste.
The question “how does laser marking improve manufacturing efficiency” can be answered through its effects on speed, cost, quality, and traceability. Laser marking reduces changeover time, lowers consumable and maintenance needs, and produces durable marks that resist wear. Clear identification improves quality control, inventory management, and product tracking throughout the supply chain. It is suitable for metals, plastics, ceramics, and other materials across industries such as automotive, electronics, medical equipment, and general manufacturing. Successful implementation requires selecting suitable equipment, configuring safe operating conditions, and matching laser settings to each material and production goal.
 Kinray Laser