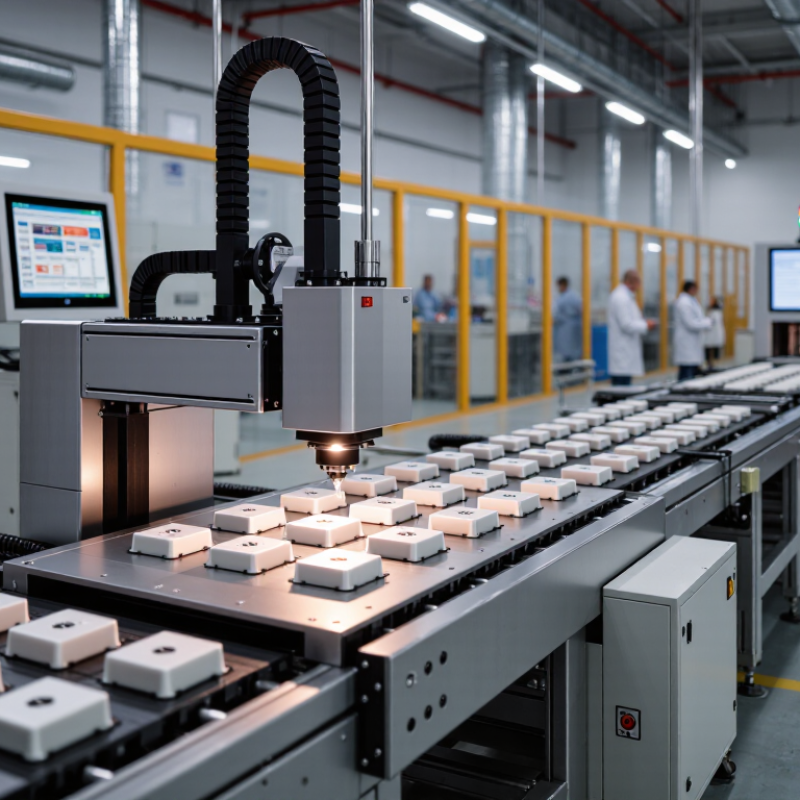
Laser marking integration connects a marking system with the machines, software, and inspection tools already used on a production line. It replaces isolated manual marking with a controlled, traceable process. Manufacturers may mark serial numbers, barcodes, logos, dates, or safety information directly onto metal, plastic, glass, and coated parts. The goal is not simply faster marking. It is consistent identification without slowing material flow.
Understanding how to integrate laser marking systems into production lines requires practical planning. Engineers must review conveyor speed, product position, marking depth, ventilation, guarding, and communication protocols. A vision camera can confirm part orientation before marking begins. A scanner can verify the code before the product moves forward. These details matter. One misplaced mark can create rework, shipment delays, or confusing quality records. Experienced integrators usually test sample parts under real production conditions, not only inside a laboratory.
Integration still has weak points. Reflective surfaces may produce uneven contrast. Dust can reduce lens performance. Software connections may fail when legacy equipment uses limited communication options. These issues deserve honest attention. A reliable system includes preventive maintenance, operator training, access controls, and documented validation checks. It should also meet applicable workplace safety and product-traceability requirements. A well-integrated laser marker becomes part of the production process, rather than an expensive device operating beside it. That difference determines whether the investment delivers dependable value.
What Laser Marking Integration Means: 1D/2D Codes, PLCs, and MES
What Is Laser Marking Integration in Production Lines?
What Laser Marking Integration Means: 1D/2D Codes, PLCs, and MES
Laser marking integration connects a marking station with the machines and software controlling production. It turns a code into a verified production record, not merely a dark mark on metal or plastic.
A 1D barcode stores data in parallel lines and suits simple identification. A 2D code stores more information in a compact square, even on limited surfaces. Data may include a serial number, batch, date, or process route. Before marking, a PLC can confirm the correct part position and recipe. It can also pause the conveyor when a sensor reports misalignment.
The details matter. A camera should read the code immediately after marking. The PLC then receives a pass or fail signal and directs the part accordingly. Meanwhile, the MES can link the serial number with the operator, machine, timestamp, and inspection results. This supports traceability across shifts and helps engineers investigate defects without guessing.
In real installations, timing is often harder than expected. A code may look clear to people but fail automated verification. Dust, vibration, changing surface finish, and incorrect focus can reduce readability. Teams sometimes validate only the laser, not the complete data chain. That is a weakness. Test records should cover rejected parts, network interruptions, duplicate serial numbers, and recovery after power loss. Leave room for improvement.
Design the Cell: 20–100 W Fiber Lasers, Sensors, Vision, and PLCs
Laser marking integration begins with the cell design, not the laser source alone.
A 20–100 W fiber laser can mark steel, aluminum, and engineered plastics at different speeds. The selected power must match material, depth, cycle time, and heat tolerance. Higher power is not automatically better.
The cell should include a rigid mounting frame, guarded access, extraction, and clear service space. A fixed focal distance helps maintain consistent contrast across every part. Sensors confirm part presence and orientation before marking starts. Vision systems can read datamatrix codes, inspect surface position, and verify the finished mark. Small lighting changes can affect inspection accuracy. This detail is often underestimated.
The PLC coordinates the sequence through clear handshakes. It receives the part-ready signal, checks safety conditions, triggers the laser, and waits for inspection results. A rejected part should move into a controlled bin, not return to production unnoticed. Use traceable recipes with locked marking parameters. Validate them with real production samples, including scratched, oily, and slightly misaligned parts. A perfect first layout is rare. Cable routing, glare, and operator access usually need revision after testing. The design should also allow lens cleaning and calibration without dismantling the entire cell. That saves time later.
Match Throughput: 10–600 m/min Lines and Sub-Millisecond Triggers
What Is Laser Marking Integration in Production Lines?
Laser marking integration connects a marking head with conveyors, encoders, PLCs, vision systems, and line controls. The goal is not merely printing faster. It is matching throughput, product spacing, and trigger timing without losing traceability. At 600 m/min, material travels about 10 meters every second. A 1-millisecond timing error can shift the mark by roughly 10 millimeters. That is already unacceptable on a small label.
The International Federation of Robotics reported 541,302 industrial robot installations worldwide in 2023. This growth reflects a wider move toward connected production, where marking must respond to real-time data. On a 10 m/min line, a sensor may offer generous timing tolerance. On a 600 m/min line, the system needs stable encoder feedback, low-latency communication, and carefully tuned laser exposure. Sub-millisecond triggers matter here.
Integration also requires practical testing. Vision inspection should confirm contrast, position, and code quality before products leave the line. Reject timing must account for conveyor delay, air pressure, and product gaps. Small errors accumulate. I have seen theoretical cycle times fail when vibration loosened a sensor bracket or reflective film confused the detector. The 2024 PMMI automation outlook highlights the industry’s continued investment in connected machinery, but connectivity alone does not guarantee accuracy. A slower, well-calibrated line can outperform a faster system with unstable synchronization.
What Is Laser Marking Integration in Production Lines?
Throughput matching from 10–600 m/min with sub-millisecond trigger timing
This reference chart compares common production-line speeds with the distance a moving product travels during a 1 ms trigger window. The distance is calculated from line speed using: distance = speed × time. As throughput increases, precise encoder synchronization and low-latency triggering become increasingly important for maintaining accurate mark placement.
Verify Codes: ISO/IEC 15415, GS1 DataMatrix, and Vision-Based Grading
Laser marking integration turns a code printer into a controlled production step. On a live line, the system marks each part, triggers a camera, and records the result.
GS1 DataMatrix symbols need correct data structure, contrast, cell shape, and quiet zones. These details affect scanning after handling, coating, or mild surface wear.
ISO/IEC 15415 provides a grading framework for two-dimensional symbols. It examines symbol contrast, modulation, fixed pattern damage, and decoding performance. A high grade is useful, but it does not replace testing on the actual product.
Vision-based grading adds immediate feedback. A camera can reject blurred cells, missing marks, poor alignment, or unreadable edges within milliseconds. Production engineers should set lighting, focus, distance, and exposure before tuning the pass threshold.
In practice, shiny metal can create reflections that look like false defects. Dust can also change a grade. The system needs calibration samples, traceable records, and periodic challenge tests. One weakness remains: a passing image may still fail at a downstream scanner. That gap deserves review.
Tips:
Validate codes after realistic handling, not only beside the marker. Keep approved reference samples at the inspection station. Check grade trends, not just pass or fail. Review rejected parts manually before changing thresholds. A lower threshold may increase output, but it can hide process drift. Also confirm that encoded data matches the intended serial record. Small mismatches create serious traceability problems.
Release Safely: IEC 60825-1 Class 1, OEE, and Reject-Rate Metrics
What Is Laser Marking Integration in Production Lines?
Laser marking integration connects a marking station with conveyors, sensors, vision systems, and production software. A safe release requires more than a clear code. The enclosed system should meet IEC 60825-1 Class 1 conditions during normal operation and foreseeable faults. This means validating guarding, access doors, interlocks, beam containment, and maintenance procedures. Do not treat a supplier declaration as the complete assessment. Site conditions can change the result.
OEE provides a practical production view. Track availability during laser warm-up, performance against planned cycle time, and quality through accepted marks. A useful baseline is an 18-second cycle, with downtime recorded by cause. Reject-rate metrics should separate unreadable codes, misplaced marks, damaged surfaces, and upstream defects. This detail helps engineers correct the process instead of hiding losses in one percentage. In real installations, the first dashboard is rarely perfect. Review it after several shifts.
Tips: Photograph sample parts before approval. Test dark, reflective, curved, and contaminated surfaces. Confirm scanner readability at the line speed. Record every failed interlock test. Set an alarm for rising rejects, not only machine downtime. Train operators to stop safely and report unusual noise, heat, or enclosure damage. A small manual inspection can reveal errors that automated vision misses. Keep controlled records for risk assessments, validation results, software changes, and corrective actions. Release the line only when safety evidence and production metrics agree.
What Is Laser Marking Integration in Production Lines? - Release Safely: IEC 60825-1 Class 1, OEE, and Reject-Rate Metrics
Anonymized production-line performance dataset for integrated laser-marking release control
| Line ID |
Application |
Laser Configuration |
IEC 60825-1 Safety Class |
Takt Time
(s/unit) |
Weekly Output
(units) |
Availability
(%) |
Performance
(%) |
Quality
(%) |
OEE
(%) |
Reject Rate
(%) |
Release Gate Status |
| LM-01 |
Aluminum component traceability |
20 W fiber laser; vision verification; PLC handshake |
Class 1 enclosure |
8.0 |
18,420 |
96.8 |
97.1 |
99.6 |
93.6 |
0.42 |
Released |
| LM-02 |
Stainless-steel valve identification |
30 W fiber laser; barcode grading; MES confirmation |
Class 1 enclosure |
12.0 |
12,760 |
94.9 |
95.8 |
99.2 |
90.2 |
0.78 |
Released |
| LM-03 |
Polymer housing data matrix marking |
10 W fiber laser; camera inspection; reject diverter |
Class 1 enclosure |
6.5 |
22,180 |
97.4 |
96.2 |
98.9 |
92.6 |
0.96 |
Released |
| LM-04 |
Electrical connector serialization |
20 W fiber laser; inline scanner; ERP record lookup |
Class 1 enclosure |
5.0 |
28,940 |
92.7 |
91.9 |
99.1 |
84.5 |
1.08 |
Conditional |
| LM-05 |
Automotive bracket permanent marking |
50 W fiber laser; fume extraction; safety interlock |
Class 1 enclosure |
15.0 |
9,860 |
95.6 |
94.4 |
99.4 |
89.7 |
0.61 |
Released |
| LM-06 |
Medical-device instrument marking |
20 W fiber laser; dual image verification; audit trail |
Class 1 enclosure |
20.0 |
7,420 |
98.1 |
97.6 |
99.8 |
95.5 |
0.19 |
Released |
| Weekly portfolio summary |
99,580 |
95.9 |
95.5 |
99.3 |
90.9 |
0.67 |
5 released / 1 conditional |
OEE
Availability × Performance × Quality
Reject Rate
Rejected units ÷ total processed units × 100
Release Control
Safety validation, interlock test, marking verification, and traceability confirmation
Conclusion
Laser marking integration connects a laser workstation with the wider production system so products can receive permanent 1D or 2D codes while moving through the line. This process involves selecting a suitable 20–100 W fiber laser, coordinating sensors, cameras, and PLCs, and exchanging production data with MES platforms. When planning how to integrate laser marking systems into production lines, engineers must match marking and inspection operations to line speeds ranging from 10 to 600 m/min, using precise, sub-millisecond trigger signals to maintain accurate placement.
Reliable integration also requires code verification and safe operation. Vision systems can assess DataMatrix readability according to ISO/IEC 15415 principles and support GS1-compliant data structures, while automatic reject mechanisms remove products with missing, damaged, or incorrectly positioned marks. Finally, the cell should be designed for IEC 60825-1 Class 1 safety conditions and monitored through practical metrics such as OEE, verification results, downtime, and reject rates.
 Kinray Laser