Laser marking should produce clear, consistent results, whether it is engraving a small serial number or adding a logo to a metal part. Yet even a well-maintained machine can create faint text, uneven lines, unwanted burns, or marks that shift out of position. These defects are frustrating. They can also waste material and slow production.
This guide explores ten common laser marking problems and practical ways to investigate them. It explains how to troubleshoot common laser marking problems by checking the workpiece, focus distance, lens cleanliness, settings, and machine alignment. A blurry mark, for example, may come from incorrect focus rather than insufficient power. A dark edge can point to excessive heat, while inconsistent depth may suggest a surface or motion issue. Small checks matter.
Good troubleshooting starts with observation, not guesswork. Compare a test mark with a known-good sample, change one setting at a time, and record the result. Confirm that the material is suitable for the laser and follow the equipment manufacturer’s instructions. Some causes overlap, so the first explanation may be wrong. That happens. Careful testing helps narrow the possibilities without making several changes at once. The right adjustment depends on the laser source, material, and application; there is no universal setting that fixes every mark.
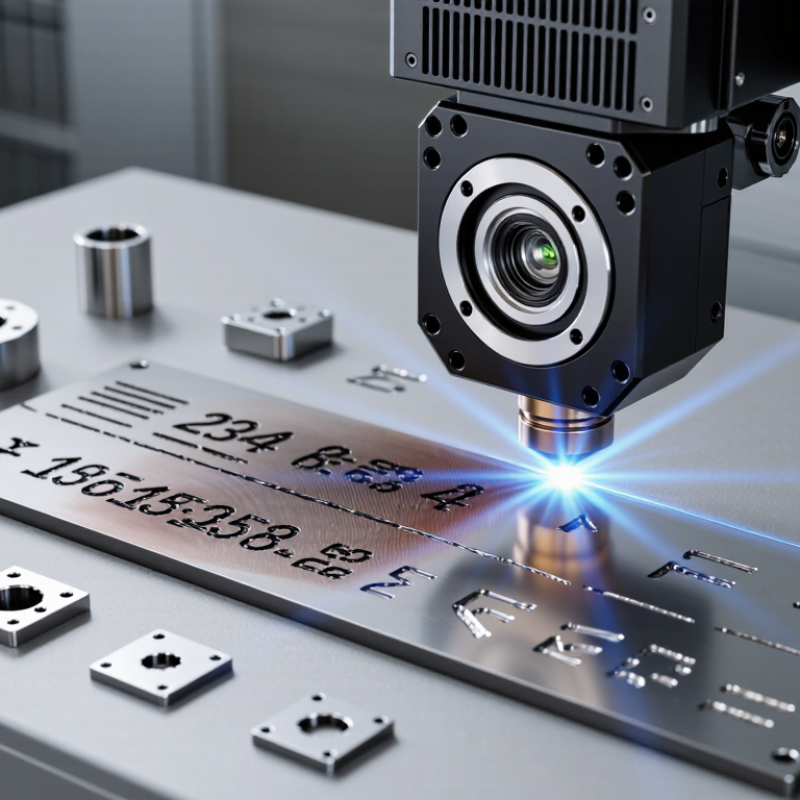
For 20–50 W, 1064 nm fiber markers, diagnose faults against measured baselines, not appearance alone. ISO 11554 specifies methods for measuring laser power and energy; ISO 11146 covers beam-width and beam-propagation measurements. These standards matter because a drifting power reading or distorted beam can mimic a software, lens, or material problem. Record output power at the work surface, focus position, scan speed, pulse frequency, and material lot before changing settings.
Small checks help. Ten recurring faults deserve attention: weak contrast, uneven fills, blurred edges, double images, missed strokes, excess heat tint, shallow marks, deep grooves, lens contamination, and unstable output.
As a practical screening benchmark, compare output with the machine’s clean, warmed-up baseline; investigate a change above 5%, rather than treating 5% as a universal failure limit. Check focus with a test grid, then inspect the protective window under angled light. A dusty window can make a clean vector look poorly aligned.
Keep a dated sample card for each material and setting. Use a loupe to compare line width and edge quality, and a calibrated meter for power checks. If results vary between runs, inspect fixture movement and part height before raising power.
That fix is sometimes overlooked. These shop-floor thresholds are diagnostic prompts, not published universal tolerances; the ISO measurement standards define methods, not guaranteed marking quality. I would still recheck the baseline after service, because one tidy test piece can hide a drifting machine.
Blur, focus drift, and weak contrast often come from small setup changes, not a failing laser. Dust on the protective window can soften edges, while a tilted workpiece shifts the focal plane across the marking area. Clean the optics with approved materials, then secure a flat sample at the correct working distance. Check the beam with a simple test pattern. Look closely at fine lines and small text.
For repeatable focus, use a calibrated height gauge or focus tool and aim to hold the surface position within ±0.05 mm, where the machine and material allow it. That figure is a setup target, not a guarantee for every system. Mark a grid at the center and corners; compare line width and darkness under consistent lighting. If contrast fades toward one edge, inspect lens seating, field alignment, and workpiece level before increasing power. More power can hide the symptom while widening marks or heating the part. I have seen a “fixed” setting fail after a fixture was replaced. Annoying, but useful evidence. Record the distance, lens condition, material, and test result, then repeat after any mechanical change.
The chart ranks common optics and focus-related marking problems by their typical impact on contrast, edge definition, and dimensional accuracy. Correct focus positioning should remain within ±0.05 mm for stable fine marking.
How to read it: Higher impact scores indicate a greater risk of blurred edges, drifting mark position, weak contrast, or inconsistent line width. Start with focus offset, lens contamination, beam alignment, and workpiece flatness before changing laser power or speed.
Material and wavelength must be matched before changing software settings. In production trials, 1064 nm usually marks bare metals efficiently, while 355 nm often gives cleaner results on plastics, glass, and thin coatings. A 532 nm source can suit colored surfaces and delicate parts, but its performance depends strongly on absorption and surface finish. These are practical starting points, not fixed rules.
Frequency changes the energy delivered by each pulse. At 10 kHz, pulse energy is often higher, which can improve depth but increase melting or burrs. At 100 kHz, marks may appear smoother and faster, yet contrast can weaken. Pulse width matters just as much. Shorter pulses generally reduce heat spread, while longer pulses may create broader thermal damage. Inspect the edge under magnification.
Use a small test grid before full production. Keep focus, scan speed, hatch spacing, and power controlled while testing 355, 532, or 1064 nm settings. Then compare contrast, depth, surface texture, and heat discoloration. I have seen operators blame the wavelength when the real problem was poor focus. A clean first pass is not guaranteed. Materials also vary between batches, so one successful setting may need adjustment. Record every result, including failed marks, because those failures often reveal the usable process window.
Laser marking inconsistency often starts with motion, not the laser source. Loose fixtures, dirty guide rails, or vibration can shift a mark between passes. Check the workpiece clamp and inspect the motion path before changing power settings. Small shifts matter.
To approach ±0.01 mm repeatability, measure the same reference feature across repeated runs, at a stable temperature and with the same fixture. Treat that figure as a verified operating target, not a guaranteed result for every material or setup.
Software issues can look mechanical. Confirm the job file, scale, origin, and correction settings before production. A mistaken field size or outdated parameter can move artwork or distort dimensions.
Run a test grid on a sample piece, then compare it with a calibrated measuring tool. Keep records. Include the machine settings, material, and measured deviation; without those details, troubleshooting becomes guesswork. Even experienced operators sometimes change several settings at once. That makes the real cause harder to find.
Routine maintenance protects uptime. Clean lenses and rails using approved procedures, check cable connections, and listen for new motor noise. Schedule inspections during planned pauses, and keep common wear parts available.
Track stoppage causes rather than counting only total downtime. A 99% uptime goal depends on the measurement period, workload, and maintenance schedule. Small facilities may not reach it every month, and that is worth examining.
Review recurring faults, then adjust the maintenance interval based on actual wear, not habit.
Class 4 laser marking needs more than a warning sign. The beam and reflected light can injure eyes or skin, while hot debris may create a fire risk. Enclose the marking area, test interlocks before operation, and control access during setup. Keep reflective tools and loose metal away from the beam path. Use suitable extraction for marking fumes. Protective eyewear must match the laser’s wavelength and exposure risk; it is not a substitute for an enclosure. Small checks matter.
Mark quality needs its own controls. ISO 9001 supports documented, repeatable quality processes, but it does not define whether a particular mark is acceptable. Set clear criteria for readability, contrast, position, and dimensions. Inspect a first-off sample, then verify marks at a risk-based frequency and after changes to material, focus, or settings. Check with the intended scanner or reader, not just by eye. A mark can look sharp and still be unreadable. Record inspection results, machine settings, batch details, and measurement-device calibration status so defects can be traced. In a busy shop, these records can feel like extra work; skipping them makes later investigations harder.
| No. | Problem | Why It Matters | Practical Fix | Verification and Records |
|---|---|---|---|---|
| 1 | Accessible Class 4 laser radiation | Direct or reflected beam exposure can cause serious eye or skin injury. A system’s classification depends on its configuration and accessible emissions. | Use a suitable beam enclosure, interlocked access points, controlled access, and documented operating procedures. Do not bypass safety devices. | Have a competent person assess the installed configuration and accessible emissions. Record the assessment, enclosure checks, interlock tests, and corrective actions. |
| 2 | Incorrect or unsuitable laser eyewear | Protective eyewear must be appropriate for the laser wavelength and the hazard. General-purpose safety glasses may not provide laser protection. | Select eyewear using a documented hazard assessment. Check wavelength range, optical density, condition, fit, and compatibility with the task. | Keep eyewear specifications, inspection records, and user training records. Replace damaged eyewear and follow the manufacturer’s instructions. |
| 3 | Uncontrolled specular reflections | Reflective metals and polished surfaces can redirect the beam into unexpected areas, including outside the intended work zone. | Assess the workpiece and fixture, control beam direction, use suitable barriers, and avoid placing reflective objects in the beam path. | Document the work-area assessment and confirm controls during setup checks, especially when materials, fixtures, or beam paths change. |
| 4 | Interlocks are bypassed or not tested | A defeated or failed interlock can allow operation when an enclosure or access point is open. | Prohibit routine bypassing. Use a controlled maintenance process for any necessary service override, with authorization and restoration checks. | Test interlocks at defined intervals and after maintenance. Record the test result, equipment status, technician, and any repair or retest. |
| 5 | Inadequate fume and particulate extraction | Marking may produce fumes or fine particles depending on the material and process. Exposure and contamination risks vary by application. | Assess the materials and process, provide suitable local exhaust ventilation, and follow safe handling and disposal procedures. | Maintain extraction inspection and service records. Verify airflow or other specified performance checks and review controls when materials change. |
| 6 | Marks are inconsistent or unreadable | Low contrast, incomplete characters, poor positioning, or variable depth can make identification and traceability unreliable. | Define acceptance criteria for content, location, contrast, legibility, and any required code format. Control the approved recipe and setup parameters. | Inspect samples against documented criteria using suitable visual or code-reading methods. Retain results and identify the accepted setup or recipe revision. |
| 7 | Marking parameters change without approval | Changes to power, speed, frequency, focus, or other process settings can affect mark quality and may create unassessed safety conditions. | Restrict parameter access and use approved settings. Evaluate and authorize changes before production use. | Keep controlled parameter versions, change approvals, trial results, and records linking the approved setup to the production lot. |
| 8 | Incorrect focus, fixture, or part positioning | Variation in focal position or workpiece location can produce weak, distorted, or misplaced marks and may alter the beam path. | Use repeatable fixtures, setup instructions, and focus checks. Confirm the part orientation and safe beam containment before marking. | Record first-piece approval and defined setup checks. Recheck after fixture changes, maintenance, or other events identified in the control plan. |
| 9 | Verification is not defined or documented | ISO 9001 requires appropriate monitoring and measurement where needed to verify conformity; it does not prescribe one universal laser-mark acceptance test. | Set measurable, application-specific acceptance criteria and inspection frequency. Define who checks the mark and what happens when it fails. | Retain inspection results, equipment or method status where relevant, nonconformity records, and disposition decisions according to the quality system. |
| 10 | Maintenance or training records are incomplete | Unrecorded maintenance, inadequate training, or undocumented safety checks can make it difficult to demonstrate that controls remain effective. | Train authorized operators and maintenance personnel on applicable procedures, hazards, emergency response, and change control. | Maintain training, preventive maintenance, safety-check, incident, and corrective-action records. Review recurring issues and verify corrective actions. |
Record power at the work surface, focus position, scan speed, pulse frequency, and material lot. Small checks help.
Dust on the protective window, incorrect focus, or a tilted workpiece can soften marks. Check the optics and surface height.
Mark a test grid at the center and corners. Compare fine lines under the same lighting.
Aim for surface positioning within ±0.05 mm where the machine and material allow it. It is not a universal guarantee.
Compare readings with a clean, warmed-up baseline. A change above 5% is a useful prompt to investigate, not a universal failure limit.
Check whether the part is level and the lens is seated correctly. A fixture change can shift the focal plane.
Not right away. More power may widen marks or heat the part while hiding the real cause.
Keep a dated sample card for each material and setting. Use a loupe to inspect line width and edges.
A tidy test piece can hide drift. Repeat the baseline check, even when the first result looks fine.
This guide explains how to troubleshoot common laser marking problems in China-made systems operating around 20–50 W at 1064 nm. It covers ten frequent faults, including blurred marks, focus drift, weak contrast, uneven lines, and inconsistent positioning. Practical checks help restore focus within ±0.05 mm and improve marking quality by reviewing the optics, workpiece setup, and process settings before replacing components.
The guide also shows how to match wavelength, frequency, and pulse width to different materials, including 355, 532, and 1064 nm systems with operating frequencies of 10–100 kHz. It addresses motion accuracy, software settings, and routine maintenance to support ±0.01 mm repeatability and dependable uptime. Finally, it outlines safeguards for Class 4 laser risks and recommends verifying mark legibility, consistency, and traceability through a documented quality process aligned with ISO 9001.
Kinray Laser