Why Are the Latest Trends in Laser Processing Important?

Time:2026-10-19 Author:Sienna
0%

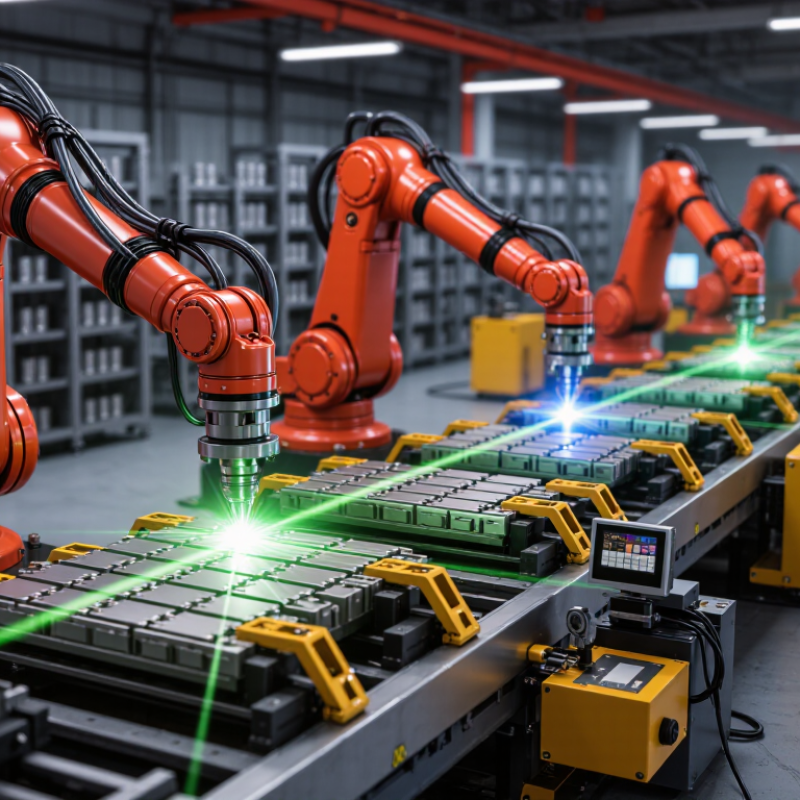
Laser processing is moving from a specialist capability into a core manufacturing investment. But what are the latest trends in laser processing technology, and why should manufacturers care now? The answer lies in measurable changes on factory floors, not fashionable terminology. Ultrafast lasers, green wavelengths, beam shaping, artificial intelligence, and robotic integration are improving control over heat, speed, and material waste. These advances matter when a hair-thin weld must remain consistent across thousands of battery cells.

The stakes are practical. According to the International Federation of Robotics’ World Robotics 2024 report, manufacturers installed 541,302 industrial robots worldwide in 2023. Laser heads increasingly operate inside these automated cells, where repeatability and real-time monitoring affect productivity. Market forecasts also indicate strong expansion. Fortune Business Insights estimates that the global laser processing market could grow from about USD 20 billion in 2023 to more than USD 40 billion by 2032. Forecasts differ, however, because researchers define “laser processing” differently.

Energy efficiency is another important driver. The U.S. Department of Energy identifies process optimization, reduced scrap, and intelligent automation as practical routes toward industrial energy savings. In a modern production line, a stable beam can reduce rejected parts, while inline vision systems can detect defects before an entire batch is affected. The picture is mixed. High-power systems remain expensive, and skilled technicians are still essential. Some factories may adopt automation too quickly and underestimate maintenance, safety training, or data quality. Therefore, the latest trends deserve careful evaluation, supported by validated trials, supplier documentation, and independent performance data rather than marketing claims.
Why Are the Latest Trends in Laser Processing Important?

Laser Processing Defined: Beam Control, Materials, and Core Methods

Why Are the Latest Trends in Laser Processing Important?

Laser processing uses a controlled beam to cut, weld, drill, mark, or surface-treat materials. Beam control determines accuracy, heat input, and edge quality. Modern systems adjust focus, pulse duration, power, and scanning speed in real time. A 50-micrometre shift can change a narrow cut into visible taper. That detail matters in electronics, medical components, and lightweight structures.

Materials respond differently. Steel absorbs energy differently from aluminum, copper, polymers, and composites. Short pulses can limit heat-affected zones, while continuous beams support deeper welding. Core methods include laser cutting, welding, ablation, cladding, and surface texturing. Grand View Research estimated the laser processing market at about $21 billion in 2023, with strong growth expected through 2030. The figure signals demand, not guaranteed performance. Factory trials still reveal costly surprises.

Tips: Start with a small material test matrix. Record power, speed, focus position, gas flow, and surface finish. Inspect cross-sections, not only the top surface. Follow ISO 11553 guidance for machine safety and laser processing risks. Reports from MarketsandMarkets also project steady market expansion, but forecasts change with energy prices and manufacturing cycles. That uncertainty deserves attention. A perfect sample may still hide unstable production.

Market Evidence: Fiber Lasers Reach 30–40% Wall-Plug Efficiency

Why Are the Latest Trends in Laser Processing Important?

Market Evidence: Fiber Lasers Reach 30–40% Wall-Plug Efficiency

Recent laser-processing trends matter because efficiency affects production cost, heat management, and equipment design. Fiber lasers can now achieve approximately 30–40% wall-plug efficiency under suitable operating conditions. This means more electrical power becomes useful laser output, while less becomes waste heat. For a busy cutting line, that difference can reduce cooling demand and improve operating stability.

The figure is not universal. Actual results depend on power level, duty cycle, beam delivery, maintenance, and material thickness. A clean optical path helps preserve performance. Dust, misalignment, or unstable cooling can quietly reduce efficiency. In practical testing, engineers should record input power, output power, ambient temperature, and processing speed. Measurements taken only from a specification sheet may look impressive, but they can miss factory conditions.

Tips: Compare energy use per finished part, not efficiency alone. Check output power at the intended operating range. Allow time for warm-up and thermal stabilization during tests. Keep cooling filters clean and inspect protective windows regularly. Also, question optimistic measurements. My own view is that 30–40% is strong market evidence, but it should not become an automatic purchasing rule. A lower-rated system may still perform better for a specific material, thickness, or production schedule. Efficiency matters. It is only one part of the process.

Precision Metrics: Micromachining Enables Features Below 10 μm

Why Are the Latest Trends in Laser Processing Important?

Precision now defines competitive micromanufacturing. Modern ultrafast lasers can create holes, slots, and channels below 10 μm. These features support microfluidic devices, sensors, medical components, and semiconductor parts. According to Grand View Research’s 2024 Laser Processing Market report, the global market was estimated at about USD 6.8 billion in 2023. Growth reflects demand for smaller, cleaner, and more repeatable parts. However, a small feature is not automatically a good feature. Taper, debris, heat damage, and edge roughness still affect performance.

On the production floor, process stability matters as much as spot size. A 7 μm opening may fail if its diameter varies across a batch. Operators should monitor pulse energy, repetition rate, focus position, and assist-gas flow. Measurement systems should verify feature width and depth after machining. Standards such as ISO 11146 also support reliable laser-beam characterization. This improves traceability, although measurement uncertainty is often underestimated. That is worth questioning.

Tips: Start with a small test matrix. Measure ten or more features, not just one. Use cross-sections when possible. Compare the first and last parts in a batch. Keep a record of material thickness, focal offset, and cleaning conditions. A slower scan may improve quality, but it can reduce throughput. The best setting is rarely the fastest one.

Why Are the Latest Trends in Laser Processing Important?

Precision Metrics: Diffraction-Limited Spot Diameter at NA = 0.50

Shorter laser wavelengths produce smaller theoretical diffraction-limited spot diameters. The values below are calculated using d = 1.22λ/NA with a numerical aperture of 0.50, showing why modern laser micromachining can support feature scales well below 10 μm. Actual feature size also depends on pulse duration, beam quality, material response, and process control.

Quality Standards: ISO 9013 Rates Thermal-Cut Edges from 1 to 5

Why Are the Latest Trends in Laser Processing Important?

Laser processing trends increasingly focus on measurable edge quality, not only cutting speed. ISO 9013 provides a common language for evaluating thermally cut surfaces. Its quality classes range from 1 to 5, with Class 1 representing the most controlled edge condition. Lower classes may show greater roughness, angular deviation, or visible heat effects. That matters.

An inspector may check a cut plate under strong, even lighting. The edge should be examined for burrs, drag lines, striations, and excessive discoloration. Measurements can include perpendicularity or angularity tolerance and average roughness. Material thickness, laser settings, assist gas, and nozzle alignment all influence the result. A clean-looking edge does not automatically meet the required class.

In practical fabrication, the specified ISO 9013 class should match the part’s function. A visible architectural panel may require tighter control than a concealed support bracket. Engineers should record material grade, thickness, cutting parameters, and inspection results. This documentation improves traceability and supports honest supplier discussions. However, visual checks alone remain limited. I have seen edges appear excellent until a roughness test revealed inconsistent bands near the lower section. That small oversight can affect coating adhesion, fit-up, or fatigue performance. Operators may also adjust settings for speed, then discover that the edge quality has quietly slipped from Class 2 toward Class 3. Standards help expose that trade-off before it becomes an expensive repair.

Industrial Impact: EVs, Semiconductors, and Aerospace Drive Adoption

Why Are the Latest Trends in Laser Processing Important?

Laser processing is becoming a practical production tool, not merely a laboratory technique. In EV factories, short laser pulses weld battery tabs, clean contact surfaces, and cut thin copper parts. The narrow heat zone helps protect nearby materials and supports compact pack designs. It also reduces mechanical force during delicate operations. Production engineers still watch spatter, distortion, and inconsistent electrical resistance. Small defects can spread through thousands of cells. That risk makes in-line cameras and power monitoring increasingly valuable. The process is fast. It is not automatically stable.

Semiconductor manufacturing creates an even stricter demand for control. Lasers can mark wafers, separate dies, drill microscopic features, and repair selected layers. Their contactless action limits tool wear and particle generation, supporting cleaner environments. However, heat accumulation may damage sensitive structures beneath the surface. Engineers therefore adjust pulse duration, wavelength, focus, and scanning speed with narrow tolerances. Reliable results require calibrated equipment, documented recipes, and repeated inspection. A promising trial is not enough. Yield data must survive real production conditions.

Aerospace manufacturers use laser cutting, drilling, cladding, and surface treatment for lightweight alloys and complex components. These methods can shorten tool paths and reduce material waste. They also help produce cooling channels and intricate structures that conventional machining may struggle to reach. Yet certification changes the conversation. Every parameter, inspection image, and repair decision may need traceability. That discipline improves confidence, but it adds time and cost. Adoption is therefore uneven. Faster processing alone does not justify a new system. Teams must balance accuracy, maintenance, operator training, and long-term repeatability. Some early assumptions will be wrong. Careful testing reveals them.

Why Are the Latest Trends in Laser Processing Important? - Industrial Impact: EVs, Semiconductors, and Aerospace Drive Adoption

Measurable process trends and industrial effects across high-growth manufacturing sectors

Table 1. Industrial relevance of major laser-processing trends
Industry Laser process and current trend Representative technical data Industrial requirement addressed Expected operational impact Adoption signal
Electric vehicles Laser welding of battery tabs, busbars, and cell connections; increased use of inline monitoring and closed-loop control. Typical weld spot or beam diameters are approximately 0.1–1.0 mm, depending on optics and joint design. Pulsed and continuous-wave systems are both used. Low electrical resistance, repeatable joints, limited heat-affected zones, and high process consistency across large battery assemblies. Higher automation potential, lower consumable use, reduced mechanical distortion, and improved traceability of weld quality. High
Electric vehicles Green-wavelength laser welding for copper and other highly reflective materials. Visible green lasers commonly operate near 515–532 nm; copper absorption is generally higher at these wavelengths than at near-infrared wavelengths around 1,030–1,070 nm. More stable energy coupling, reduced spatter risk, and better control of thin copper joints and dissimilar-material connections. Improved weld repeatability and a wider process window for high-volume battery and power-electronics production. High
Semiconductors Laser dicing and scribing of wafers, advanced packages, and brittle substrates; greater use of ultrashort pulses. Ultrashort-pulse systems typically use pulse durations from femtoseconds to picoseconds. Laser kerf widths can be in the tens-of-micrometres range, depending on material and process conditions. Minimal chipping, low mechanical force, narrow kerfs, and compatibility with thin or fragile wafers. Higher usable die yield, reduced post-processing, and greater design flexibility for smaller device geometries. High
Semiconductors Laser annealing and selective thermal processing for dopant activation and thin-film manufacturing. Processing can range from nanosecond pulsed heating to millisecond-scale scanning, concentrating thermal energy near the surface rather than heating the entire substrate. Localized thermal budgets, reduced substrate distortion, and processing of materials that are sensitive to prolonged furnace exposure. Supports advanced device architectures, shorter thermal cycles, and improved compatibility with thinner substrates. Growing
Aerospace Laser powder-bed fusion for lightweight structural parts, thermal components, and complex internal channels. Typical metal powder-bed layer thickness is approximately 20–60 µm; commonly reported laser powers range from roughly 100–1,000 W, depending on the material and system. Complex geometry, part consolidation, weight reduction, and production of geometries that are difficult to machine conventionally. Lower material waste, fewer assembled components, shorter design-to-production cycles, and potential mass reduction. High
Aerospace Laser directed-energy deposition and cladding for repair, remanufacturing, and localized material addition. Typical deposited bead widths are approximately 0.5–3 mm, with deposition rates varying widely according to powder or wire feedstock, material, and part geometry. Restoration of high-value parts, controlled material placement, and reduced need to replace complete components. Lower repair material consumption, extended component service life, and reduced downtime for selected maintenance operations. Growing
Cross-industry Inline optical sensing, machine vision, and artificial-intelligence-assisted process monitoring. Monitoring variables may include reflected light, plasma emission, melt-pool geometry, temperature, acoustic signals, and dimensional measurements. Early detection of porosity, lack of fusion, overheating, spatter, misalignment, and dimensional drift. Reduced inspection delays, stronger process traceability, and movement from end-of-line inspection toward real-time quality assurance. Very high
Cross-industry Higher-power fiber lasers, beam shaping, and multi-beam processing for increased throughput. Industrial continuous-wave fiber-laser systems commonly span from several kilowatts to tens of kilowatts for cutting, welding, and additive-manufacturing applications. Higher material-removal or joining rates while maintaining controlled energy distribution and manageable thermal effects. Improved equipment utilization, shorter cycle times for suitable applications, and greater scalability of automated production lines. High
Data notes: The technical values are representative published ranges rather than guaranteed equipment specifications. Actual results depend on material composition, part geometry, beam quality, optics, pulse settings, shielding, scanning strategy, and quality-control requirements.
Reference basis: Typical ranges are aligned with technical literature and industry guidance associated with ISO/ASTM 52900 additive-manufacturing terminology, semiconductor wafer-processing practices, laser-material-processing research, and public manufacturing-technology reports.

FAQS

What is laser processing?

Laser processing uses a controlled beam to cut, weld, drill, mark, or treat surfaces. Beam control affects heat, accuracy, and edge quality.

Which settings most affect processing results?

Focus position, pulse duration, power, and scanning speed matter greatly. A 50-micrometre shift can create visible taper. Small adjustments matter.

Do different materials require different laser settings?

Yes. Steel, aluminum, copper, polymers, and composites absorb energy differently. Test each material separately before production.

How can manufacturers reduce heat damage?

Short pulses can limit heat-affected zones. Continuous beams may support deeper welding. The best choice depends on material thickness and joint design.

What should a basic material test include?

Create a small test matrix. Record power, speed, focus, gas flow, and surface finish. Inspect cross-sections, not just the surface.

How are lasers used in battery production?

They can weld thin tabs, clean contact surfaces, and cut copper parts. Their narrow heat zones reduce nearby damage. Spatter still needs attention.

Why is monitoring important during production?

Cameras and power monitoring can detect unstable conditions. Small defects may affect many parts. Fast processing does not guarantee consistent results.

What challenges appear in semiconductor processing?

Sensitive layers may suffer from heat accumulation. Engineers carefully adjust wavelength, pulse duration, focus, and scanning speed. Yield data matters more than one successful trial.

Why does aerospace production require extra documentation?

Complex components may need traceable parameters, inspection images, and repair decisions. Certification adds time and cost. Faster processing alone is not enough.

Can laser processing always replace conventional machining?

No. It may reduce waste and reach intricate structures, but maintenance, training, accuracy, and repeatability still matter. Early assumptions can be wrong.

Conclusion

Laser processing is becoming a core manufacturing technology because it combines precise beam control, flexible material compatibility, and efficient non-contact methods such as cutting, welding, drilling, marking, and micromachining. When considering what are the latest trends in laser processing technology, several developments stand out: fiber lasers are achieving wall-plug efficiencies of approximately 30–40%, helping reduce energy use and operating costs, while advanced micromachining systems can create features smaller than 10 μm for highly demanding applications.

These improvements are having a major impact on electric vehicle production, semiconductor fabrication, and aerospace manufacturing, where accuracy, repeatability, and process stability are essential. Quality control is also becoming more standardized. ISO 9013 provides a clear framework for rating thermally cut edges from 1 to 5, allowing manufacturers to evaluate surface quality and process consistency more objectively. Together, higher efficiency, finer resolution, and measurable quality standards explain why modern laser processing continues to expand across advanced industries.

Sienna

Sienna

Sienna is a skilled marketing professional with a deep expertise in our company’s core products and services. With a passion for innovation and detail, she plays a pivotal role in crafting insightful blog posts that not only highlight the unique features of our offerings but also provide valuable......